| Material Type | Fused quartz or fused silica rod manufactured from high-purity silica. | Material grade must be stated clearly, including whether the rod is electrically fused, flame fused, or produced by another documented process. | Review material certificate, manufacturing declaration, and traceability records. | Do not compare quotations solely by the term “quartz.” Confirm the material process because impurity levels, bubbles, hydroxyl content, and thermal behavior can differ substantially. |
| Chemical Purity | Impurity profile appropriate for the intended application, especially alkali metals, iron, aluminum, calcium, magnesium, titanium, and copper. | Set numerical limits in the purchase specification; for high-purity optical or semiconductor-related use, limits are commonly defined in parts per million or lower according to the application. | Independent laboratory analysis using ICP-OES, ICP-MS, or an equivalent validated method. | Request a lot-specific certificate rather than a generic brochure value. The required limit should be based on process sensitivity, not only on nominal material grade. |
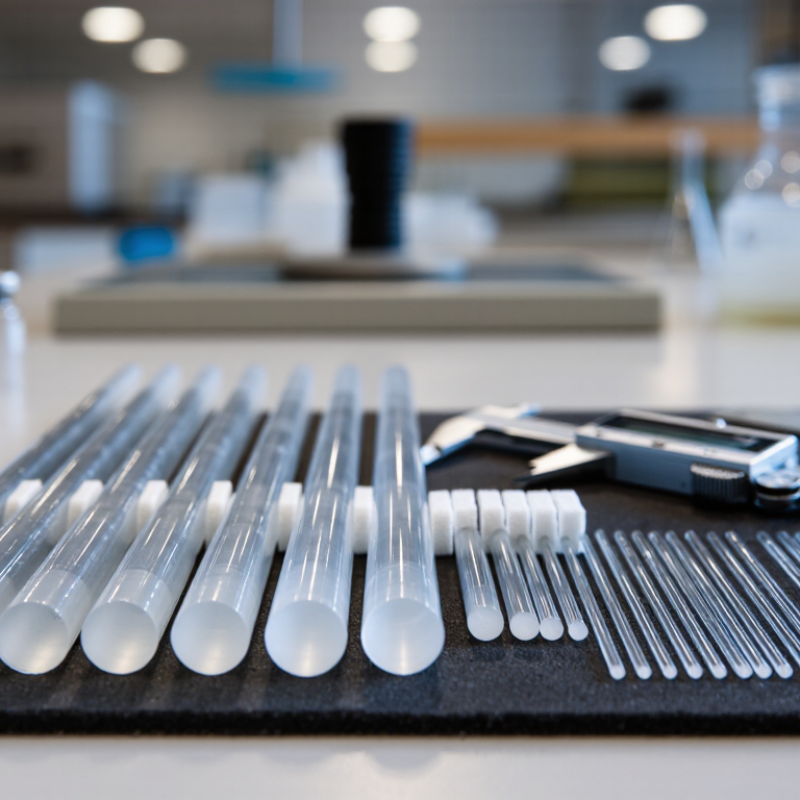
| Rod Diameter | Round rod diameter selected according to the assembly, machining allowance, and thermal load. | Typical commercial diameters may range from approximately 1 mm to more than 100 mm; define the exact nominal diameter and tolerance on the drawing. | Calibrated micrometer, optical measurement system, or coordinate measuring machine at multiple positions along the rod. | Specify measurement locations and temperature conditions. Diameter variation can affect sealing, heating uniformity, and mechanical fit. |
| Dimensional Tolerance | Diameter, length, straightness, and end geometry must be controlled according to the application. | A practical starting point for general-purpose rods is diameter tolerance of ±0.10 mm and length tolerance of ±1.0 mm, subject to drawing approval. | Inspection report based on calibrated instruments and a documented sampling plan. | Tighter tolerances may require additional grinding or polishing and should be priced separately. Avoid using “standard tolerance” without a numerical definition. |
| Length | Cut length must match the equipment design and allow for end finishing. | Define nominal length, permissible deviation, minimum usable length, and whether both ends require finishing. | Calibrated steel rule, height gauge, or optical comparator, depending on tolerance. | For international shipments, include protective end caps and specify whether quoted length is before or after end finishing. |
| Roundness and Straightness | Cross-section should remain circular and the rod should be free from visible bending. | Define maximum out-of-roundness and total indicator reading on the technical drawing; use application-specific limits rather than an undefined “round” description. | Rotational gauge measurement, laser measurement, or coordinate measurement over the full usable length. | Straightness is especially important for furnace elements, optical paths, guide components, and automated loading systems. |
| Surface Finish | Surface may be fire-polished, ground, or optically polished depending on function. | Define roughness or visual finish, for example polished, translucent, or ground; specify maximum scratches, pits, chips, and contamination. | Visual inspection under controlled lighting; profilometer measurement where a numerical roughness value is required. | A bright or transparent appearance alone does not prove a suitable surface finish. Use reference samples or approved visual standards for repeat orders. |
| Optical Transmission | Transmission range should correspond to ultraviolet, visible, near-infrared, or infrared service. | Define the wavelength range and minimum transmission only when optical performance is relevant; results must identify sample thickness and measurement conditions. | UV-Vis-NIR spectrophotometer or FTIR spectrometer, as appropriate to the specified wavelength range. | Transmission depends on hydroxyl content, impurities, bubbles, surface condition, and thickness. Do not accept an optical value without test conditions. |
| Hydroxyl Content | OH concentration must be controlled for applications involving ultraviolet transmission, infrared transmission, vacuum, or thermal cycling. | Set an application-specific maximum, commonly expressed in parts per million by mass or by an agreed spectroscopic classification. | Infrared spectroscopy or another validated supplier or third-party method. | Low-OH and high-OH fused silica behave differently during heating and in spectral transmission. State the required OH range explicitly. |
| Bubbles and Inclusions | Rod must be free from unacceptable bubbles, cords, stones, devitrification, and foreign inclusions. | Define maximum bubble size, total bubble count, inclusion type, and inspection zone; use zero-tolerance only where technically justified. | Visual inspection with transmitted and reflected light, supported by magnification or imaging when necessary. | Acceptance criteria should distinguish cosmetic marks from defects that can initiate fracture or distort optical and thermal performance. |
| Thermal Performance | Low thermal expansion and resistance to thermal shock are required for rapid heating and cooling. | Use a documented coefficient of thermal expansion requirement; fused silica is commonly specified at approximately 0.5 × 10⁻⁶ K−1 near room temperature, subject to grade and test range. | Dilatometry according to an agreed method and temperature range. | Never use a single expansion value without stating the temperature interval. Thermal shock performance also depends on geometry, surface defects, and heating rate. |
| Maximum Service Temperature | Operating temperature must be compatible with the rod geometry, load, atmosphere, and exposure duration. | Fused silica softening temperature is approximately 1,680°C, but continuous-use limits must be set below the softening range and validated for the specific design. | Review technical data and conduct application-specific thermal testing where continuous high-temperature service is critical. | High temperature can cause deformation, devitrification, or surface contamination even when the nominal softening temperature is not reached. |
| Mechanical Condition | Rod must withstand handling, machining, assembly, and expected service loads without unacceptable cracks or chips. | No through-cracks, harmful edge chips, or deep grinding damage; mechanical strength requirements should be defined by application and geometry. | Visual inspection, polarized-light stress inspection, and application-specific mechanical testing. | Quartz is brittle and surface flaws strongly influence strength. Specify handling controls and reject criteria for damage introduced after production. |
| Annealing and Internal Stress | Internal stress should be minimized through controlled thermal processing. | No visible abnormal birefringence or stress pattern under a suitable polarized-light inspection for components requiring thermal or mechanical stability. | Polariscopic inspection under documented lighting and viewing conditions. | Stress inspection is valuable for detecting processing problems that may not be visible under ordinary white light. |
| Cleanliness | Products must be free from oil, dust, abrasive residue, fingerprints, packaging fibers, and process chemicals. | Define allowable particulate level, cleaning chemistry, and whether cleanroom packaging is required. | Visual inspection, wipe testing, particle counting, or surface analysis according to end-use risk. | For vacuum, optical, laboratory, and semiconductor-related applications, cleanliness requirements should be written as a separate controlled specification. |
| End Finishing | Ends may be square-cut, chamfered, fire-polished, ground, or polished. | Specify end angle, chamfer width, edge sharpness, chip size, and allowable heat-affected zone. | Visual inspection and dimensional measurement using magnification where required. | Improper end finishing can create crack initiators and may interfere with seals, holders, or subsequent machining. |
| Packaging | Packaging must prevent impact, abrasion, moisture-related contamination, and movement during transport. | Individual sleeves or separators, cushioned inner packaging, rigid outer cartons or crates, and clear orientation markings for long rods. | Packaging inspection before dispatch and photographic evidence of packed goods. | Request shipment protection appropriate to the rod length and fragility. Packaging damage should be recorded before acceptance. |
| Traceability | Each shipment must be traceable to a production lot and inspection record. | Lot number, production date, material grade, quantity, inspection status, and certificate reference must appear on the packing list and product label. | Document review and label-to-certificate reconciliation. | Maintain traceability from purchase order through incoming inspection and final use. Mixed lots should not be accepted without prior approval. |
| Quality Management | Supplier should operate a documented quality-management system suitable for the risk and application. | Request evidence of a current ISO 9001-based quality system or an equivalent documented process; regulated applications may require additional sector controls. | Certificate review, supplier questionnaire, remote audit, or on-site audit. | Certification does not replace product inspection. Verify that the certified scope covers the relevant glass or quartz-processing activities. |
| Inspection Sampling | Incoming inspection should cover dimensions, appearance, documentation, and any critical chemical or optical properties. | Use a written sampling plan based on lot size, defect severity, supplier history, and application risk; critical defects should have zero acceptance where justified. | Inspection records using calibrated equipment and approved defect definitions. | Use tightened inspection for first articles, new suppliers, process changes, or repeated nonconformities, then adjust only with documented evidence. |
| Applicable Standards | Testing and quality requirements should reference recognized methods where available. | Potential references include ISO 9001 for quality management, ISO/IEC 17025 for testing-laboratory competence, ASTM E228 for thermal expansion, and ASTM E438 for laboratory glassware material classifications where applicable. | Confirm the latest applicable edition and ensure the selected method matches the product and intended use. | Standards should support the specification, not replace it. Always state the exact edition, test method, specimen condition, and acceptance limit in the purchase documentation. |